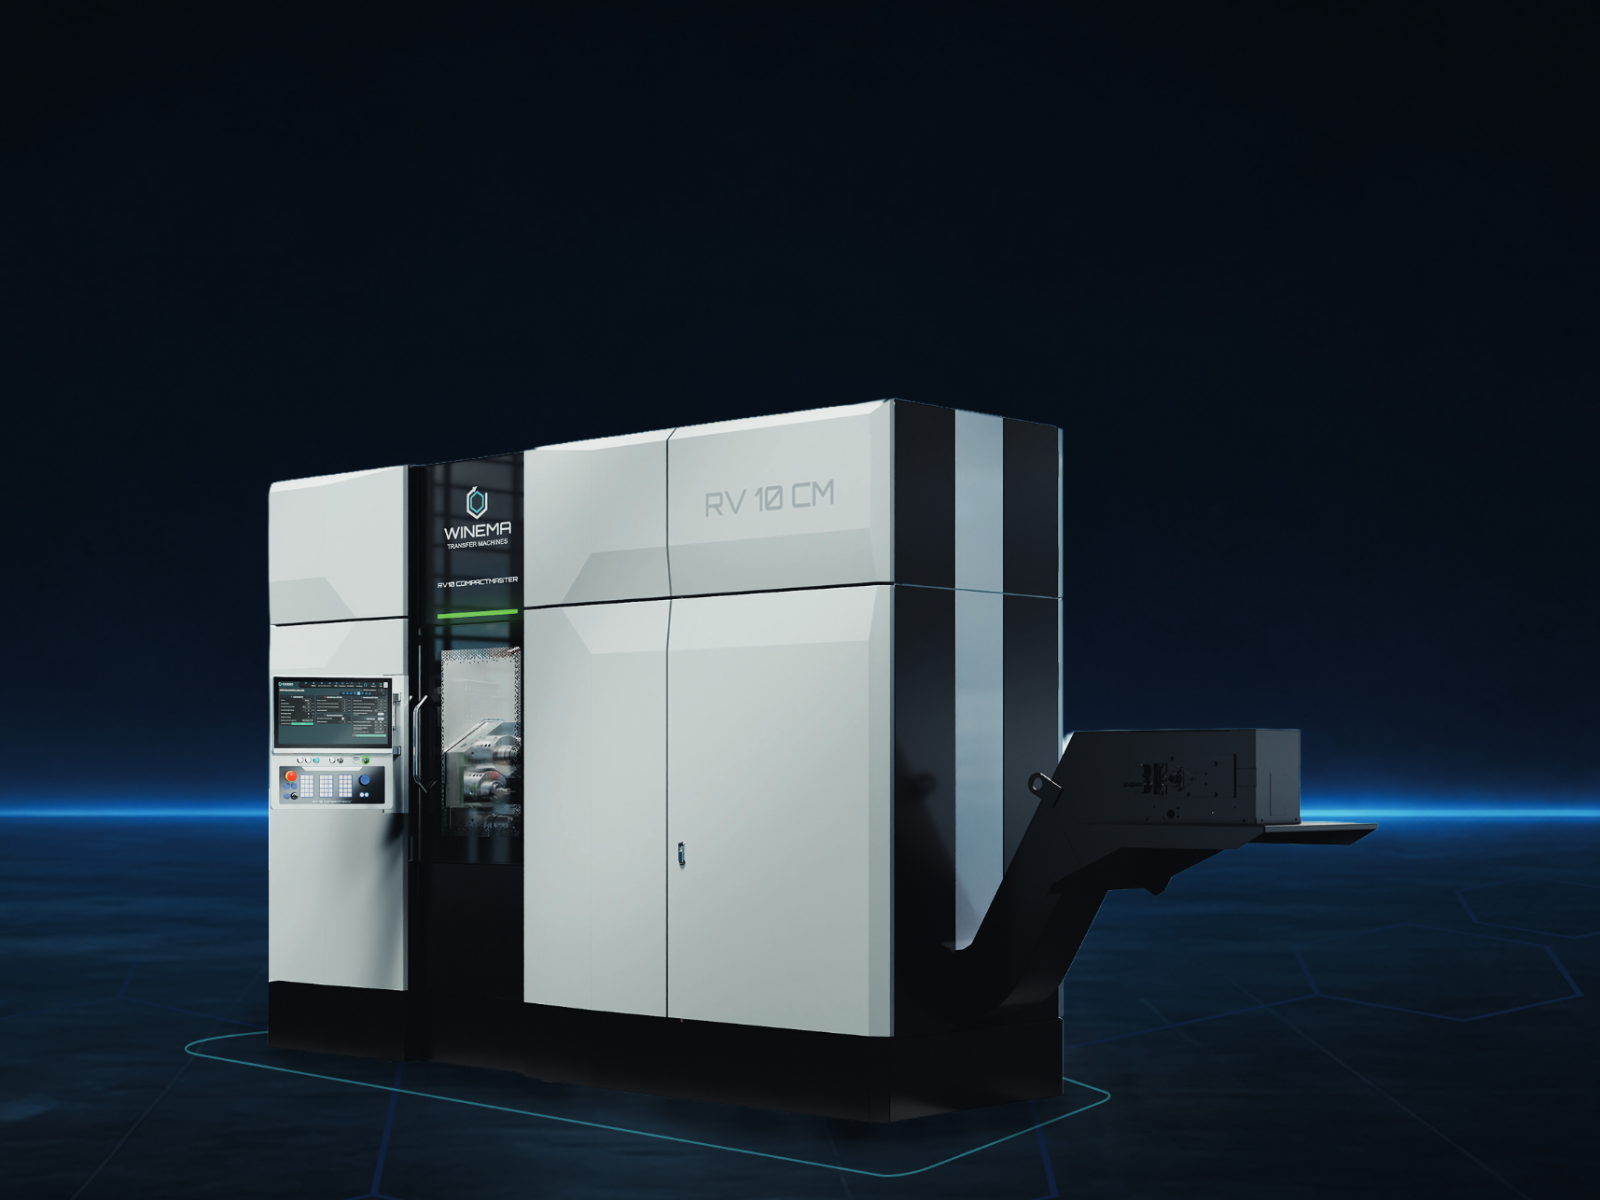
Even short workpieces with complex external contours are clamped securely and precisely. External contours can be machined directly from the bar at the pre-turning station, immediately before the workpiece is transferred to the self-centering two-jaw chuck on the indexing table. No additional reclamping or repositioning is required. Complete machining from three sides, with five axial machining stations on each side and two radial stations, ensures maximum flexibility and highest productivity.